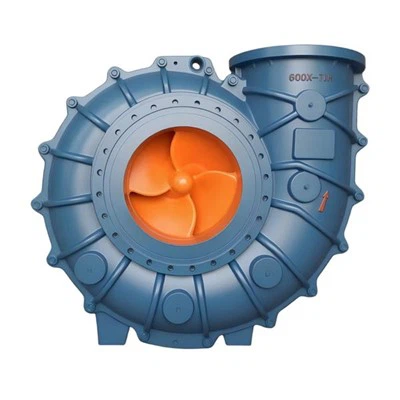
If you’ve ever stood next to an FGD pump during a plant shutdown—listened to that sharp, cracking, gravel-like noise that isn’t part of normal operation—you know cavitation isn’t just a mechanical buzzword. It’s the silent (and loud) killer of pump performance, reliability, and profitability. As someone who’s spent the last 12 years as part of a team that designs, tests, and services FGD pumps, I’ve seen cavitation turn a $50,000 pump into $100,000 in repair costs, unplanned downtime, and lost production in a matter of months. What makes it so frustrating is that most cavitation issues aren’t flukes—they’re preventable. Today, I’m breaking down the science behind why cavitation happens in FGD pumps, and the practical, field-proven steps we recommend to stop it dead in its tracks. FGD Pump

First, let’s ground this in how FGD systems work, because that context is non-negotiable. FGD (Flue Gas Desulfurization) pumps handle a brutal, unique fluid: a slurry of limestone or lime, water, fly ash, and spent flue gas pollutants, often at temperatures between 120°F and 160°F, and at pressures that can swing wildly as the plant adjusts to load. This slurry isn’t like water—it’s dense, abrasive, and prone to vaporizing under specific conditions. Cavitation occurs when the pressure at the pump’s suction inlet drops below the vapor pressure of the slurry, forming tiny vapor bubbles. When these bubbles get carried into the high-pressure zone of the pump’s impeller, they collapse violently, creating shock waves that erode the impeller, casing, and seals, and generating that dreaded noise I mentioned earlier. The result? Reduced flow, lower efficiency, and frequent breakdowns that throw the entire FGD system (and the plant’s ability to meet emissions regulations) off balance.
A common mistake I see plant operators make is blaming “bad pump design” right away. Sure, some poorly sized or mismatched pumps will cavitate, but 70% of the issues we troubleshoot are tied to suction system flaws, not the pump itself. Let’s start with the single most critical specification for preventing cavitation: Net Positive Suction Head Required (NPSHr) vs. Net Positive Suction Head Available (NPSHa). NPSHr is a pump’s inherent need for pressure at its suction inlet—each pump model has a specific NPSHr, published in our engineering data. NPSHa is the actual pressure delivered to that inlet by your suction system. The golden rule is simple: NPSHa must be at least 10% higher than NPSHr to prevent cavitation. I’ve seen this rule ignored so many times: a plant with a 1,000 gpm FGD pump that was sized for 800 gpm, so they throttled the discharge valve to slow it down, which dropped suction pressure and made NPSHa fall below NPSHr. That pump was toast in 12 months.
To improve NPSHa, there are a handful of actionable steps, starting with suction line sizing and layout. Too many plants use a suction line that’s the same size as the pump’s suction nozzle, but slurry flows more slowly in larger-diameter lines, which reduces velocity and prevents pressure drop. For FGD pumps, we always recommend a suction line one size larger than the pump inlet, with a maximum velocity of 5 feet per second (fps) for limestone slurry—any higher, and you’ll get friction-related pressure loss that crushes NPSHa. Another layout mistake is sharp elbows, tight turns, or partially closed valves within 10 feet of the pump suction. These create turbulence that lowers local pressure and leads to cavitation even if your overall NPSHa is correct. We often suggest using long-radius elbows (3D or 5D, not standard 1D) and avoiding any fittings that cause flow disruption near the suction inlet. One recent project at a coal plant in Ohio had a cavitation issue that took us three days to trace: they had a gate valve fully open but installed backward, creating a vortex that pulled air and low-pressure slurry into the pump. Reversing the valve fixed it immediately.
Next up, pump selection: not all FGD pumps are created equal, especially when it comes to cavitation resistance. A standard centrifugal pump for clean water won’t cut it for slurry FGD applications. We design our FGD pumps with two key features to fight cavitation: low-NPSHr impellers and rugged, wear-resistant materials. The impeller is the heart here—we use closed impellers with large, smooth flow paths to minimize turbulence and reduce the NPSHr. We also balance impellers to within 0.001 ounces, so there’s no vibration that could amplify pressure fluctuations at the suction. Materials matter too: FGD slurries are both corrosive (the sulfuric acid byproduct) and abrasive (limestone particles), so we use high-chrome iron or rubber-lined impellers and casings. Rubber, in particular, is great for dampening the shock waves from collapsing vapor bubbles—we’ve tested rubber-lined pumps that showed 60% less cavitation-related wear than all-chrome pumps in the same FGD application. That said, even the best pump won’t work if it’s mismatched to your flow rate. Avoid over-sizing pumps—it’s a common shortcut that leads to operating far below the pump’s best efficiency point (BEP), which shifts the impeller’s pressure profile and increases NPSHr demand. Always size your pump to operate at or near BEP for your average flow rate, with room for 10-15% peak load, not 50% extra capacity “just in case.”
Suction reservoir design is another area that’s easy to overlook, especially for absorption loop pumps that draw from a spray tower sump. Vortexing in the sump is a huge cavitation trigger. If the sump’s suction inlet is too close to the bottom of the tank, or the inlet velocity is too high, air gets pulled into the pump, which combines with vapor bubbles to make cavitation even worse. We recommend installing anti-vortex baffles in the sump, and keeping the suction inlet at least twice the pipe diameter above the sump bottom, and three times the pipe diameter below the sump liquid level during normal operation. If your plant is short on space, a suction diffuser or a primer tank can help—these devices smooth out slurry flow before it reaches the pump, reducing turbulence and improving NPSHa. One power plant in Pennsylvania had a sump that was only 4 feet deep, so their suction inlet was too close to the bottom and they had constant vortexing. Adding a 12-inch tall anti-vortex baffle eliminated the noise and cut pump wear by 80%.
Operating practices also play a massive role in preventing cavitation. Plant operators often prioritize keeping emissions in spec over pump maintenance, but small, consistent adjustments can make a huge difference. First, monitor NPSHa and NPSHr in real time—most modern pump control systems can track suction pressure, flow rate, and slurry temperature, so you can spot when NPSHa is dropping below the 10% threshold before cavitation starts. If you’re running multiple pumps in parallel (common in FGD systems for redundant capacity), make sure they’re all matched for flow rate and NPSHr. Uneven loading means one pump will be pulling more flow, which drops its suction pressure and causes cavitation. We’ve seen parallel pumps set up with a single throttle valve on the suction line, leading to 20% higher flow through one pump and constant cavitation. Instead, use individual suction isolation valves for each pump to adjust flow evenly. Slurry temperature is another key variable—higher temperatures raise the vapor pressure of the slurry, so NPSHa drops by about 0.3 psi for every 1°F increase in temperature. If your plant’s FGD loop is running too hot (above 160°F), that’s a red flag—check for heat from the flue gas entering the absorber, or insufficient cooling water in the loop. Lowering slurry temperature by 5°F can improve NPSHa enough to eliminate cavitation in many cases.
Maintenance is the final line of defense. Cavitation causes wear that becomes a vicious cycle: as the impeller erodes, its flow path changes, increasing NPSHr, which makes cavitation worse, and so on. Schedule regular inspections every 6 to 12 months (depending on run time) to check for cavitation damage: pitting on the impeller and casing, cracked seals, or unusual play in the shaft. If you spot pitting, don’t just grind it out—replace the impeller if the damage is deeper than 1/8 inch, because grinding can leave uneven surfaces that cause more turbulence. We also recommend testing the pump’s NPSHr annually, either in our in-house test lab or in the field, to make sure it’s still within specification as wear occurs. Another maintenance tip: prime pumps properly during start-up. Many operators skip priming steps for redundancy, but running a pump with air in the suction line will cause immediate cavitation. For pumps that sit idle for more than 24 hours, bleed air from the suction line before starting.
I’ll be honest—cavitation is never completely eliminated 100% of the time, but it can be reduced to levels that keep your FGD pump running for 5+ years instead of 1 or 2, and avoid the unplanned shutdowns that cost plants tens of thousands of dollars per hour. The key is to treat cavitation prevention as a system, not just a pump problem: get the suction right, size and select the pump for your application, adjust operating practices, and stay on top of maintenance. If you’re struggling with cavitation in your FGD pumps, or you’re looking to upgrade your system to reduce downtime, our engineering team has worked with hundreds of power plants and industrial facilities to troubleshoot and implement solutions that work in real-world, high-demand conditions. We don’t sell one-size-fits-all pumps—we work with your specific FGD loop, flow rates, and site constraints to create a plan that fits your needs and budget. Whether you need a full pump replacement, a minor suction line modification, or regular pump performance audits, we’re here to help you get your FGD system running reliably and efficiently.
Sand Pump References
- Karassik, I. J., McGuire, R. L., & Messina, J. P. (2008). Pump Handbook (4th ed.). McGraw-Hill.
- American National Standards Institute. (2014). ANSI/HI 9.6.1-2014 Rotodynamic Pumps for NPSH Margin. Hydraulic Institute.
- Huisseune, H., et al. (2017). Cavitation in centrifugal slurry pumps: A review of experimental and numerical investigations. Wear, 376-377, 1532-1544.
- Limestone FGD System Design Guidelines. (2020). Electric Power Research Institute (EPRI).
Shijiazhuang Ruite Pump Co., Ltd.
Shijiazhuang Ruite Pump Co., Ltd. is one of the most experienced FGD pump manufacturers and suppliers in China. Please rest assured to wholesale high quality FGD pump made in China here from our factory. For price consultation, contact us.
Address: Majuan village, Nandong town, Gaocheng, Shijiazhuang, China
E-mail: info@ruitepump.com
WebSite: https://www.rtslurrypump.com/
